No products in the cart.
Cubicles and Office Furniture
Buying Bulk Office Cubicles: 25 to 200 Workstations Without Surprises
14
Sep
Sep
Buying four workstations and buying two hundred are not the same activity at a larger scale. Above roughly twenty stations the constraints change: freight becomes truckload rather than parcel, installation becomes a scheduled project rather than an afternoon, dye lots and production runs start to matter, and the difference between a good and a bad unit price compounds into five figures.
This guide covers what actually changes when you buy bulk office cubicles, where the volume savings genuinely come from, how to structure the order so it arrives in the right sequence, and the specification decisions that are expensive to reverse once two hundred of something are on a truck.
Where volume pricing actually comes from
It is worth understanding the mechanics, because it tells you which levers to pull in a negotiation and which requests simply cannot be granted.
Production batching. A factory running 200 identical panels in one setup produces them far more cheaply than 200 panels in eleven different sizes and four fabrics. Most of the real discount on bulk office cubicles comes from standardising the specification, not from asking for a better price on a varied one.
Freight efficiency. A full truckload costs less per station than four LTL shipments, and it also arrives with less handling damage. The break-even is usually somewhere around 25 to 40 stations depending on configuration.
Installation efficiency. An installer’s day rate spread over 25 stations costs far less per station than the same crew doing six. Mobilisation is a fixed cost.
Single-source overhead. One order, one project manager, one delivery schedule, one invoice. Splitting a floor across three suppliers to save 4 percent on one line item usually costs more than it saves in coordination.
The practical rule: standardise ruthlessly on panel sizes and finishes, vary only where the work genuinely differs, and buy the whole floor from one source in one production run. That combination is worth more than any discount you can negotiate on a fragmented order.
How volume changes the unit price
| Order size | Freight mode | Typical unit price movement | Install cost per station |
|---|---|---|---|
| 1 – 8 stations | LTL, often two shipments | List | $250 – $400 |
| 9 – 24 stations | LTL, consolidated | 5 – 12 percent below list | $200 – $320 |
| 25 – 60 stations | Full truckload | 12 – 22 percent below list | $165 – $260 |
| 61 – 150 stations | Multiple truckloads, phased | 20 – 30 percent below list | $140 – $220 |
| 150+ stations | Dedicated production run | 25 – 35 percent below list | $120 – $190 |
Those ranges assume a standardised specification. A 100-station order with nine panel widths, three heights and four fabrics will price closer to the 25-station band, because the factory gains nothing from the volume.
Specification decisions that are expensive to reverse
Panel height, decided once for the whole floor
Mixing heights across a floor is fine when it is planned – lower panels at the windows, taller on the phone-heavy runs – and chaotic when it is decided station by station. Settle on a primary height for the floor and at most two exceptions with a clear rule for where each applies.
Footprint, decided from measured area
On bulk office cubicles the footprint decision is the largest single financial lever in the project, because it multiplies. Moving 120 stations from 6×6 to 5×5 typically saves 15 to 25 percent of the furniture cost and frees enough floor for 15 to 25 more seats, which may remove the need for additional space entirely.
Fabric and laminate, ordered in one dye lot
Textile dye lots vary. Ordering 200 panels across two production runs three months apart can produce a visible difference in the same room under the same lighting. If the project is phased, order the fabric for all phases at once even if the panels ship later.
Power specification, set by the electrical design
Circuit count per run, base feed locations and the number of whips need to be decided with whoever is doing the electrical design, before the furniture order is placed. Changing this after delivery means new harnesses on a large scale. See our guide to cubicle installation, power and data.
Ten percent spare parts
Order roughly 10 percent extra on the small consumable parts – top caps, end trim, connectors, cantilever brackets – as part of the original run. They are cheap now and expensive to chase in two years. This is the single most common regret on large orders.
Phasing delivery so the floor is never blocked
A 150-station order does not arrive in one delivery, and you would not want it to – there is nowhere to put it. The sequence that works is delivery by zone, matched to the installation schedule.
| Phase | What arrives | Why in this order |
|---|---|---|
| Pre-delivery | Layout drawings approved, electrical rough-in complete | Panels cannot be set over unfinished floor boxes |
| 1 | Zone A panels, tops, brackets, power components | One zone only; keeps the floor clear |
| 2 | Zone B, delivered as Zone A install completes | Crew moves straight on, no idle day |
| 3 | Remaining zones, same pattern | Storage cost avoided entirely |
| Final | Accessories, spare parts, punch list items | After stations are set and measured |
The cost of getting this wrong is storage. A truckload in a rented warehouse runs several hundred dollars a month, plus double handling, plus the damage that comes with it. Sequenced delivery avoids the whole category.
The documents to insist on for a bulk order
On a small order a quote is enough. Above roughly 25 stations, ask for five things in writing before the deposit.
A full bill of materials. Every panel by width and height, every worksurface, every bracket, connector, cap and power component, with counts. This is the document you will check the delivery against.
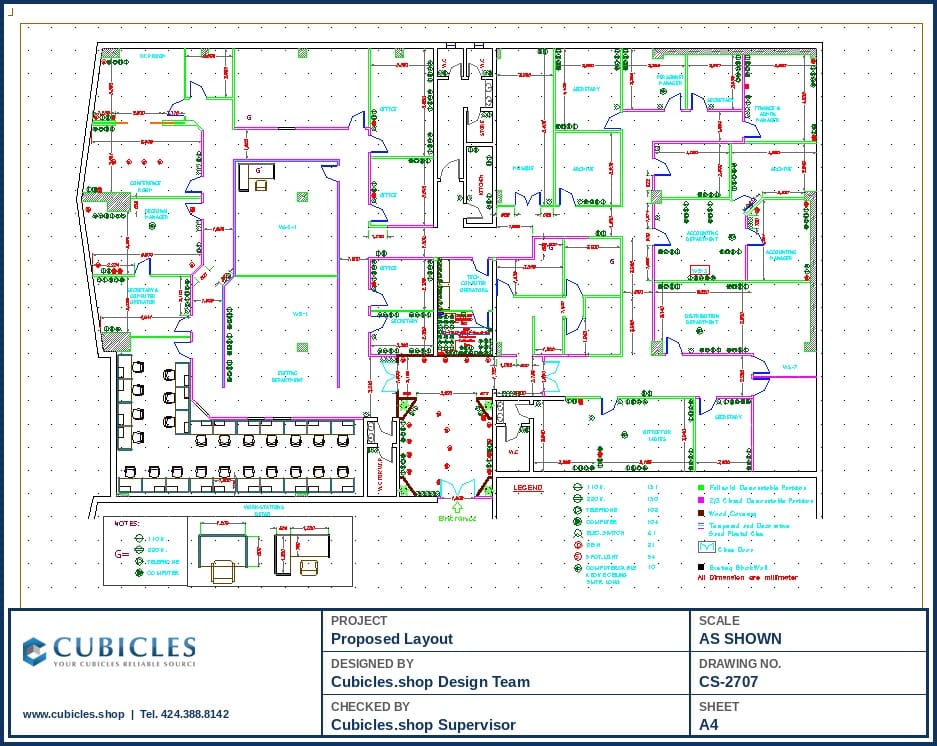
A dimensioned layout drawing. Showing the stations on your actual floor plate, with aisle widths, power feed locations and any obstruction noted.
A delivery schedule by zone. Dates, truck counts, and what is on each truck.
Freight terms. Delivered or not, liftgate or dock, inside delivery or kerb, and who signs.
Warranty terms and a parts availability statement. How long the product line will remain available for matching add-ons.
Installation on a large floor
A competent crew sets roughly 10 to 20 stations per day once mobilised. For a 120-station project, expect a crew of four to six over eight to twelve working days, usually split across zones and often including a weekend to reduce disruption.
Three things reliably cause delays. Electrical rough-in not finished when the first truck arrives – the most common. Floors that are not level, which is not exotic; older buildings routinely have half an inch of variation across a run, and levellers only have so much travel. And building access rules: loading dock hours, elevator reservations and union requirements in some buildings can halve a crew’s productive day if they are discovered on the morning of delivery rather than two weeks before.
Budgeting a bulk project
| Line | Per station | 120-station example |
|---|---|---|
| Workstations, standardised spec | $650 – $1,400 | $78,000 – $168,000 |
| Freight, truckload, phased | $55 – $120 | $6,600 – $14,400 |
| Installation | $140 – $220 | $16,800 – $26,400 |
| Electrical whips and tie-in | $60 – $140 | $7,200 – $16,800 |
| Spare parts, 10 percent of small items | $20 – $60 | $2,400 – $7,200 |
| Accessories – bins, pedestals, monitor arms | $150 – $400 | $18,000 – $48,000 |
| All in | $1,075 – $2,340 | $129,000 – $281,000 |
The accessory line is the one most often left out of an early budget and the one most likely to be blamed later. Include it from the start.
Frequently asked questions about bulk cubicle orders
What order size qualifies for volume pricing?
Meaningful movement generally starts around 25 stations, where the order fills a truck and the installation crew runs efficiently. Below that, the saving comes from product choice rather than volume.
How long does a large order take?
In-stock product for 100 plus stations typically ships in two to four weeks, phased. Made-to-order runs six to twelve weeks before the first truck. Add one to three weeks for installation depending on zone count.
Can I phase a bulk order across budget years?
Yes, and it is common. Order the full specification at once so fabric and laminate come from one dye lot, then schedule delivery and invoicing across the periods you need. Confirm the tax treatment of each phase with your accountant, since the deduction generally follows when each phase is placed in service.
Will I be able to buy matching stations in two years?
Only if the product line is in production and the supplier will say so in writing. Ask the question explicitly before ordering bulk office cubicles – it is the difference between adding six matching desks and starting a new neighbourhood.
Should I standardise on one workstation size?
Mostly yes. One primary size for the majority of staff plus one larger size for managers covers nearly every floor and keeps the production run efficient. More than two sizes rarely earns its cost.
Who manages the project?
On orders of this size the supplier should provide a single point of contact who owns the bill of materials, the delivery schedule and the installation coordination. If nobody on the supplier side owns those three things, you will end up owning them.
Price your floor
Send us the floor plate dimensions, the headcount by role, and your target date. For large runs start with 7-plus-man configurations and 6-man clusters, or browse the design layouts library to see full floor arrangements with station counts worked out. Manufacturer-direct pricing on the full cubicle range means the volume saving stays with you rather than with a dealer.